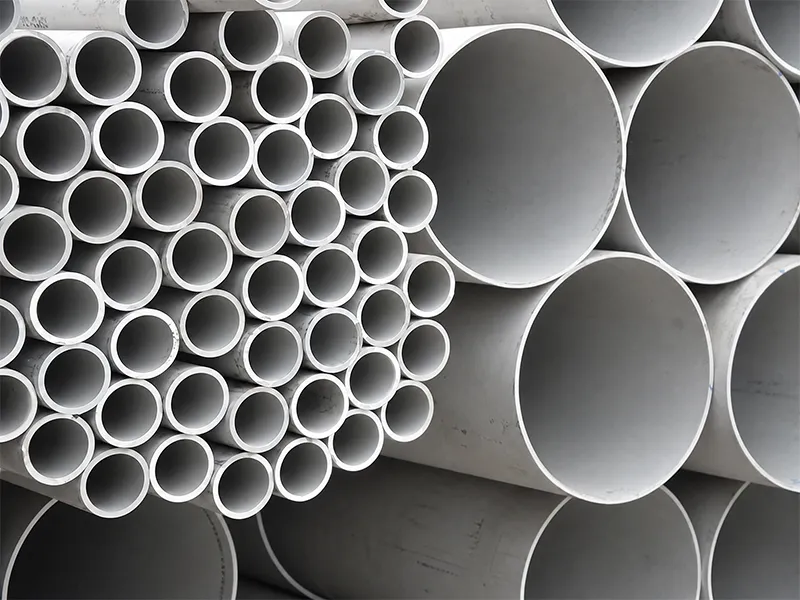
When sourcing stainless steel piping for pharmaceutical, food & beverage, chemical and industrial projects, one question our customers ask most often: seamless pipe or welded pipe?
Neither option is universally “better”. The selection depends on operating pressure, temperature, corrosive media, sanitary requirements, applicable standards and pipe size. The best choice is determined by your service conditions and budget.
This guide explains how each pipe is manufactured, their ideal applications, and six core differences between seamless and welded pipe. We also cover strength, cost, available sizes and surface finish to help you make an informed purchasing decision.
What is Seamless Pipe?
Seamless pipe is a hollow tube made from a solid steel billet with no welded joints. The billet is heated, and a mandrel pierces its centre. This process creates a uniform grain structure across the entire cross-section of the pipe.
Without a weld seam, seamless pipe withstands higher pressure and temperature than welded pipe of the same material grade and wall thickness. It is manufactured to ASTM A312 standard for stainless steel.
What is Welded Pipe?
Welded pipe starts as a flat steel strip or steel plate. The strip is rolled into a cylindrical shape, and the edges are joined by welding methods including Electric Resistance Welding (ERW), Submerged Arc Welding (SAW) or laser welding.
A visible seam runs along the pipe length. This weld line can act as a potential stress concentration point and requires extra testing and inspection. Welded pipe is a practical choice for low-to-medium pressure applications such as water distribution, structural supports and railings.
Welded pipe is available in larger diameters than seamless pipe. It is widely adopted for sizes above NPS 24 (610 mm OD), as the piercing process cannot produce such large bore sizes.
Six Key Differences Between Seamless and Welded Pipe
1. Manufacturing Process
Seamless pipe is produced by hot extrusion or rotary piercing of a solid billet. No welding is involved at any production stage.
Welded pipe is formed by rolling a flat strip and welding along the longitudinal seam. Post-Weld Heat Treatment (PWHT) may be applied to the weld seam to restore its corrosion resistance.
2. Pressure Rating & Strength
Seamless pipe has a higher pressure rating thanks to its continuous, unbroken grain structure around the circumference, with no Heat-Affected Zone (HAZ).
Welded pipe features a HAZ at the weld seam. The microstructure in this zone differs from the base metal. Under high pressure or cyclic loading, the weld seam is the most probable failure location.
For example, ASTM A312 TP316L seamless pipe with Schedule 80 wall thickness can handle a working pressure over 3000 psi (20.7 MPa) at ambient temperature. The welded variant of the same grade applies a weld efficiency factor of 0.85, lowering its pressure rating by 15%.
3. Cost Comparison
Welded pipe costs 20%–40% less than seamless pipe of identical size and grade. Flat strip raw material is cheaper, and the forming process consumes less energy.
Seamless pipe requires more raw material and additional processing steps. Piercing, elongating and sizing all add up to higher costs. Choose seamless pipe only when your application demands it, not as the default option.
4. Size & Wall Thickness Range
Welded pipe covers a broad diameter range: from NPS 1/8 (6 mm OD) up to NPS 80+ (2032 mm OD).
Seamless pipe typically ranges from NPS 1/8 (6 mm OD) to NPS 24 (610 mm OD), with wall thickness options from Schedule 5S through Schedule XXS (extra heavy). We supply heavy-wall seamless stainless pipe with thickness up to 60 mm.
5. Surface Finish & Tolerances
Seamless pipe comes with tighter OD and wall thickness tolerances compared to welded pipe. The rotary piercing method delivers a smooth internal bore free of weld beads.
Welded pipe may carry internal weld beads that need grinding or removal. The typical OD tolerance for welded pipe is ±1%, while seamless pipe is ±0.75%.
Seamless pipe provides a cleaner internal surface for instrumentation, heat exchangers and sanitary service.
6. Non-Destructive Testing (NDT) Requirements
Seamless pipe is inspected via Ultrasonic Testing (UT) or Eddy Current Testing (ECT) to detect internal defects such as inclusions and voids.
To guarantee weld integrity, welded pipe requires Radiographic Testing (RT) or Ultrasonic Testing (UT) focused on the weld seam. For critical service conditions, 100% inspection of the weld zone is mandatory.
When to Use Seamless Pipe?
Select seamless pipe for these five scenarios: • High-pressure service — boilers, pressure vessels, hydraulic lines above 2000 psi • High-temperature service — superheater tubes, furnace components above 500°C (932°F) • Corrosive environments — offshore platforms, chemical processing, sour gas (H₂S) service • Safety-critical applications — nuclear piping, subsea pipelines, LNG transfer pipelines • Small-bore instrumentation piping — below NPS 2, where weld beads restrict fluid flow
When to Use Welded Pipe?
Select welded pipe for these four scenarios: • Structural & construction applications — handrails, frames, support columns • Water and drainage systems — municipal water supply, wastewater treatment • Large-diameter pipelines — transmission lines larger than NPS 24 • Budget-conscious projects — general service with moderate pressure and temperature
Conclusion
Seamless pipe excels in pressure rating, mechanical strength and corrosion resistance. Welded pipe offers advantages in cost efficiency and large-diameter availability.
Pick seamless pipe for high-pressure, high-temperature and corrosive working conditions. Welded pipe is well suited for structural, low-pressure and cost-sensitive projects.
Contact us for a quotation if you need premium seamless stainless steel pipe.